Experience & Vision

2026 Best Roll Stock Machine Types for Global Buyers

Choosing the right roll stock machine in 2026 requires more than comparing speed, price, or supplier reputation. Global buyers must examine material compatibility, production volume, packaging formats, labor skills, and local service support. A machine running smoothly in Germany may perform differently in Indonesia, Brazil, or South Africa because of power standards, humidity, film quality, and operator training.

This guide reviews major roll stock machine types used across modern packaging and converting operations. It considers vertical and horizontal form-fill-seal systems, flow wrapping equipment, slitting and rewinding machines, laminating lines, and flexible printing solutions. Each type serves a different production need. Some machines prioritize fast output, while others provide tighter control over seals, film tension, registration, or changeover time. Small details matter. A worn roller, unstable web tension, or poorly calibrated sensor can create thousands of defective packs.

Real purchasing decisions are rarely perfect. No machine fits every factory. A lower-cost model may seem attractive, yet spare-part delays can stop production for days. An advanced line may offer impressive automation, but it could exceed the skills of a small operating team. Buyers should request test runs, inspect sample products, verify technical certificates, and speak with existing users where possible. Supplier claims deserve careful checking. This overview provides a practical, evidence-focused starting point for evaluating machine types, ownership risks, and long-term production value in different global markets.
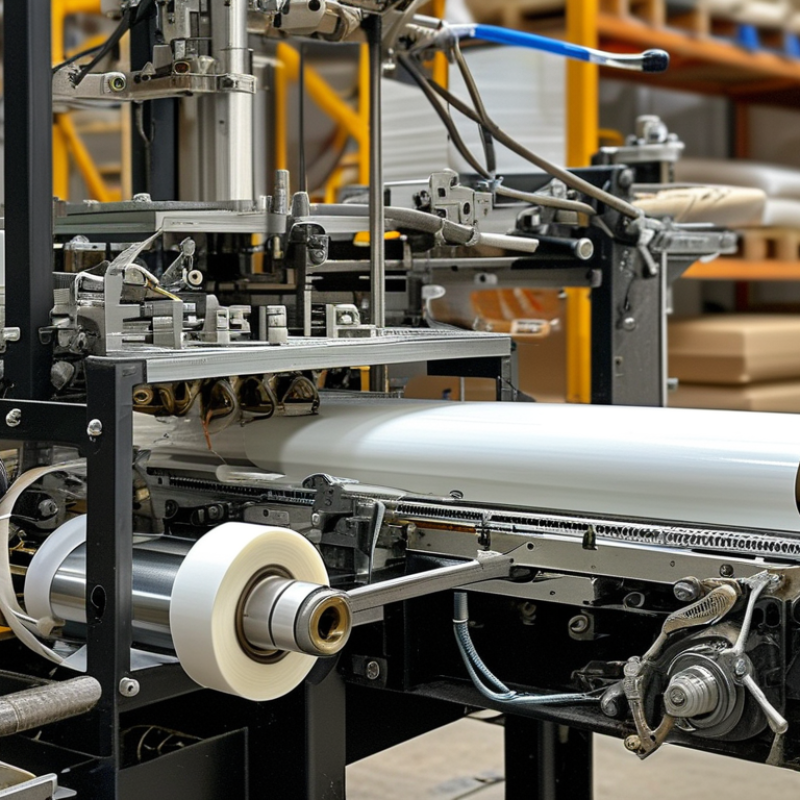
2026 Best Roll Stock Machine Types for Global Buyers

Roll Stock Machine Types: Forming, Slitting, Laminating, and Rewinding

2026 Best Roll Stock Machine Types for Global Buyers

Roll stock processing begins with the right forming machine. It shapes film, paper, or flexible laminate into consistent web structures. Operators should check forming pressure, temperature control, and material compatibility before production. Small tension errors can create wrinkles, weak edges, or uneven thickness.

Slitting machines then divide wide rolls into narrower widths for packaging and industrial use. Clean knives matter. Poor alignment often causes dust, rough edges, and telescoping rolls.

Laminating machines bond multiple layers with adhesive, heat, or pressure. They need stable tension and accurate curing control. A reliable system should support the required substrate combination and final application.

Rewinding machines convert processed webs into finished rolls with controlled hardness and even edges. Core size, winding speed, and taper tension affect storage and downstream performance.

In my experience, a fast machine is not always the best machine. A slightly slower setup may reduce waste and operator corrections. No setup is perfect. That deserves honest review.

Tips: Match each machine with the material’s thickness, width, and surface treatment. Request trial runs using your actual roll stock. Measure splice quality, roll density, edge alignment, and waste percentage. Also inspect cleaning access and safety controls. These details often matter more after installation.

calc

Core Specifications: 300–1,500 mm Widths and 50–600 m/min Speeds

2026 Best Roll Stock Machine Types for Global Buyers

Global buyers should match roll stock machines to film behavior, not catalog promises. A 300–1,500 mm web width covers compact sachets, multipacks, and wide-format packaging. Speeds from 50–600 m/min support different production realities. Mordor Intelligence’s 2024 Flexible Packaging Market report estimates the sector will grow at about 4.9% annually through 2029. That growth increases pressure to choose flexible, measurable equipment.

For narrow rolls, intermittent-motion machines can improve registration and reduce material waste. Wider 1,000–1,500 mm systems need stronger web control, stable tension, and accurate edge guiding. At 50–150 m/min, operators may prioritize fast changeovers and simple maintenance. At 300–600 m/min, servo synchronization, automatic splicing, and tension response become more important. PMMI’s 2024 packaging trends research highlights automation, labor efficiency, and sustainability as continuing investment drivers.

Speed alone is not performance. A thin recyclable film may wrinkle at high speed, even when the machine reaches its rated 600 m/min. Seal temperature, unwind diameter, ink coverage, and humidity can change the result. Smithers’ flexible packaging outlook also emphasizes material development and converting efficiency. Buyers should request trials using actual substrates. The listed width may be accurate, but usable width can shrink after edge trim and registration allowances. That detail is easy to miss.

2026 Best Roll Stock Machine Types for Global Buyers

Core specifications: 300–1,500 mm web widths and 50–600 m/min rated speeds

The chart compares representative industrial specifications by machine type. Web width indicates the maximum roll or substrate width, while rated speed represents the typical production-line speed. Actual performance varies with substrate, material thickness, print process, drying method, and converting configuration.

Material Compatibility: Steel, Aluminum, Films, Foils, and 20–200 μm Webs

2026 Best Roll Stock Machine Types for Global Buyers

Material compatibility should lead every roll stock machine decision. Steel demands rigid frames, high forming force, and stable gap control. World Steel Association reported 1.88 billion tonnes of crude steel production in 2024, showing the scale of this market. For thin steel strip, four-high or six-high mills can improve flatness and thickness control. However, heavier equipment increases energy use and installation requirements.

Aluminum needs gentler tension control. The International Aluminium Institute recorded 72.8 million tonnes of primary aluminum production in 2024. Its lower density and softer surface can create dents, scratches, or edge damage. Precision rolling and slitting systems should include polished contact surfaces, adjustable tension, and reliable web tracking. Small errors become visible quickly.

Films and foils require a different approach. Flexible packaging represented a major share of global packaging demand in recent Smithers market assessments, while film gauges commonly range from 20 to 200 μm. Air flotation, clean rollers, and low-tension unwinding help protect delicate webs. Foil is less forgiving. It wrinkles suddenly. A machine may process steel successfully but fail with 20 μm film. I have seen specifications overlook humidity, core size, and splice strength. That is a costly omission. Buyers should request trial runs using their actual material, width, coating, and target speed. Testing is slower, but guessing is worse.

Global Buyer Standards: CE, UL, ISO 9001, and 0.1 mm Tension Control

For global roll-stock buyers, machine selection begins with material behavior, not catalog speed. Slitter-rewinders suit precise web conversion, while laminators and pouch machines demand tighter registration control. Flexible packaging remains a major manufacturing sector. Smithers’ market outlook projects continued growth in flexible packaging through 2028, increasing pressure on waste reduction and repeatable output.

CE marking confirms conformity with applicable European requirements; it is not a universal quality certificate. UL evaluation is often requested for electrical safety in North American projects. ISO 9001 addresses the manufacturer’s quality-management system. The ISO Survey of Certifications 2023 recorded 1,265,216 ISO 9001 certificates worldwide. That figure shows broad adoption, but certification alone does not guarantee accurate rolls.

A serious buyer should request test records for 0.1 mm tension control across acceleration, stopping, and splice conditions. Check actual roll samples, edge quality, pneumatic stability, and sensor calibration dates. PMMI’s 2024 State of the Industry report identifies labor availability and automation pressure as important packaging investment drivers. That supports automated tension control, yet automation can hide poor setup practices. Ask for training records and fault-response procedures. Small details matter. A machine may claim 0.1 mm control, but inconsistent substrate thickness can still create wrinkles, telescoping, or uneven winding. Performance data should be verified under your own film, paper, or foil conditions.

2026 Selection Metrics: Output, Automation, Energy Use, and Total Cost of Ownership

Choosing a roll stock machine in 2026 requires more than comparing advertised speed. Output must mean saleable material per hour, not theoretical web speed. Ask for trial data using your actual substrate, width, thickness, and tolerance targets. A machine rated at 120 meters per minute may deliver 82 after changeovers, trimming, and rejects. That gap matters. Real output is quieter.

Automation should reduce decisions, not hide them. Check automatic tension control, recipe storage, splice handling, alarm history, and remote diagnostics. Operators still need clear access and manual override. A complex interface can slow a trained team during a jam. Review changeover time with two shifts, not one demonstration operator. Record minutes, scrap kilograms, and repeated faults across several production runs. Good data beats confident claims. Be skeptical.

Energy use belongs in the purchase model. Request measured kilowatt-hours per finished ton at normal load, including heaters, drives, compressors, and standby periods. Compare that figure with maintenance hours, spare-part availability, tooling life, training, downtime, and disposal costs. Total cost of ownership should cover five to ten years, with sensitivity tests for electricity prices and utilization. One weakness remains: buyers often underestimate cleaning and calibration labor. That assumption can distort payback. Have an independent engineer verify acceptance tests, safety controls, service access, and lifecycle estimates before signing.

2026 Best Roll Stock Machine Types for Global Buyers – 2026 Selection Metrics: Output, Automation, Energy Use, and Total Cost of Ownership

Machine Type Typical Applications Material Thickness Typical Line Speed Indicative Output Automation Level Typical Connected Load Estimated Energy Use Indicative 5-Year TCO Best Fit for Global Buyers
Manual or Entry-Level Roll Former Simple roofing panels, trims, light-duty channels, and low-volume custom profiles 0.30–1.20 mm steel
0.40–1.00 mm aluminum
8–15 m/min Approximately 350–750 m² per 8-hour shift, depending on profile length and handling Manual feeding and stacking; basic variable-speed control; manual length measurement or simple stop control 15–30 kW Approximately 8–18 kWh per operating hour USD 70,000–150,000 Start-ups, maintenance departments, regional fabricators, and buyers prioritizing low entry cost
Semi-Automatic Roll Forming Line Roofing sheets, wall panels, purlins, framing sections, cable trays, and standard construction profiles 0.40–2.00 mm steel
Up to approximately 1.20 mm aluminum
15–30 m/min Approximately 700–1,500 m² per 8-hour shift Powered decoiler, PLC-based controls, automatic measuring, and powered or hydraulic cutting; manual coil changes are common 25–55 kW Approximately 15–35 kWh per operating hour USD 130,000–280,000 General-purpose manufacturers requiring a balance between investment, flexibility, and productivity
Fully Automatic Servo-Controlled Line High-volume panels, structural sections, door components, modular construction parts, and repeat production 0.50–3.00 mm steel
Material limits depend on yield strength and profile geometry
25–50 m/min Approximately 1,200–2,500 m² per 8-hour shift Automatic decoiling, servo feeding, encoder-based length control, hydraulic or flying shear, recipe management, and automatic stacking options 45–90 kW Approximately 25–60 kWh per operating hour USD 280,000–650,000 Export-oriented plants and manufacturers with stable orders, high utilization, and strict dimensional requirements
Cassette Quick-Change Roll Former Multiple profiles produced on one line, including roofing, siding, framing, and industrial sections 0.40–2.50 mm steel
Profile-dependent
20–45 m/min Approximately 1,000–2,200 m² per 8-hour shift Interchangeable roll cassettes, digital setup recipes, reduced changeover time, and optional automatic length control 30–75 kW Approximately 18–45 kWh per operating hour USD 220,000–520,000 Contract manufacturers and plants serving varied regional standards or frequent small batches
High-Strength Structural Roll Former Automotive components, warehouse frames, solar support sections, heavy-duty purlins, and structural profiles 1.50–4.00 mm high-strength steel
Material strength must be validated before purchase
10–30 m/min Approximately 600–1,500 m² per 8-hour shift Heavy-duty powered entry, servo roll forming, automatic monitoring, hydraulic punching, and programmable cutting 55–120 kW Approximately 35–85 kWh per operating hour USD 400,000–900,000 Buyers requiring repeatable forming of thicker or higher-yield-strength materials rather than maximum line speed
Integrated Punching and Cutting Line Perforated channels, cable management systems, framing components, solar mounting rails, and pre-punched structural parts 0.80–3.00 mm steel
Commonly galvanized or pre-painted coil
15–40 m/min Approximately 900–2,000 m² per 8-hour shift, subject to hole pattern and punch frequency Automatic coil feeding, CNC or servo punching, synchronized forming, programmable cut-to-length, and data-recording functions 50–110 kW Approximately 35–80 kWh per operating hour USD 350,000–800,000 Plants seeking to eliminate secondary drilling, reduce handling, and supply ready-to-install components
Flexible Multi-Profile Production Cell High-mix, low-to-medium-volume production where several widths, materials, or profile families are required 0.50–2.50 mm steel
Material and profile range depends on tooling design
12–35 m/min Approximately 700–1,800 m² per 8-hour shift Digital job scheduling, recipe-based setup, automatic width adjustment options, barcode or ERP integration, and assisted changeover 35–85 kW Approximately 22–65 kWh per operating hour USD 300,000–750,000 Global buyers serving diverse construction codes, customized orders, and multiple export markets
How to read the figures: The values are indicative engineering ranges for 2026 procurement planning, not guaranteed machine specifications. Actual output depends on profile geometry, coil width, material yield strength, thickness, cut length, punching frequency, setup time, operator skill, and uptime. Energy figures refer to machine electricity consumption during production and exclude factory HVAC, compressed-air generation, lighting, and upstream material processing.
Total Cost of Ownership assumption: The five-year TCO ranges are planning estimates that combine purchase price, standard tooling, commissioning, routine maintenance, consumables, electricity, and typical production downtime. They exclude land, building work, taxes, financing, labor, raw material, freight variations, major accidents, and exceptional tooling redesign. A buyer should request a supplier-specific calculation using local electricity rates, duty rates, service costs, and annual operating hours.
Selection principle: For most buyers, the lowest purchase price is not the lowest TCO. Compare usable output per shift, changeover time, automation reliability, spare-parts availability, energy consumption per finished square meter, tooling life, local technical support, and the expected utilization rate.
Go to Top